We help retailers, brands, importers and distributors develop smarter outdoor storage products — from market insight and product design to engineering validation and launch support.
Manufacturing Capabilities
Built in-House, Measured at Every Stage
Four material streams, eleven product families and a documented QC checkpoint at every transfer between processes — from coil and billet through to sealed export packaging.
30+
Custom & standard production lines
20+
QC checkpoints per unit
16
In-house processes
50+
Export markets served
Three Material Streams
Each stream runs its own validated route. Select a material to view the production sequence and the inspection gate applied at each stage.
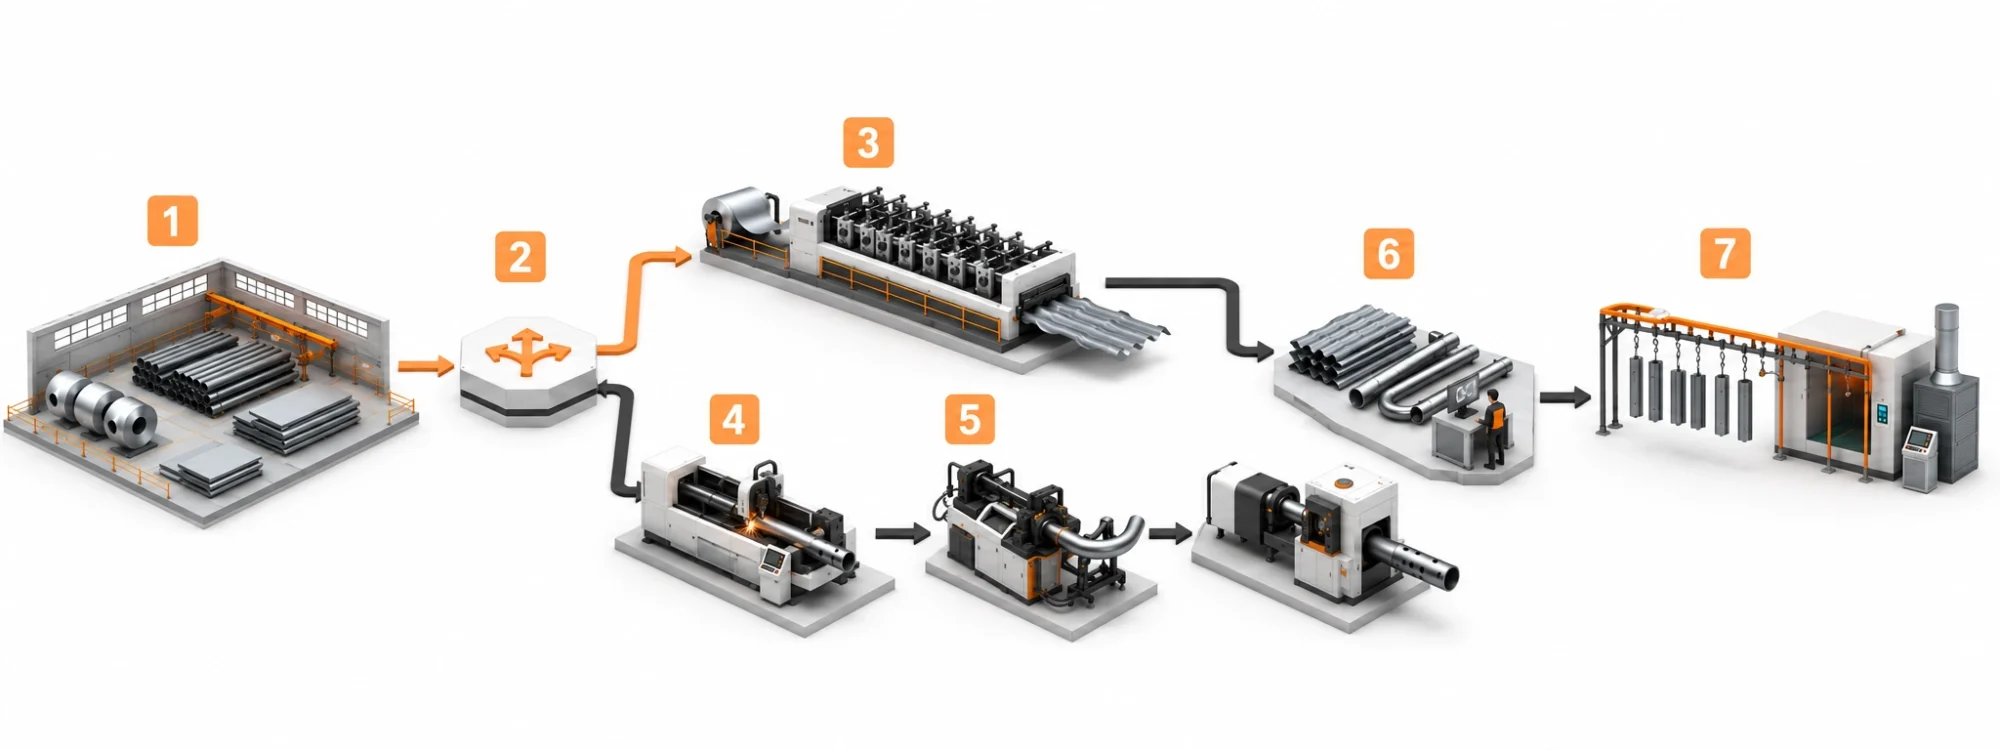
01
Material Intake
Raw material is split into two synchronised streams — sheet to panel forming, tube to cutting — so both run in parallel and converge for assembly.
02
Parallel Routing
Raw material is split into two synchronised streams — sheet to panel forming, tube to cutting — so both run in parallel and converge for assembly.
03
Milling & Deburring
Cut bars go to the drill-mill machine for finish machining, and the saw edge is deburred in the same pass — so nothing sharp or ragged carries through to assembly or to the customer’s hands. Sheet is fed through the roll former to produce corrugated roof and wall panels in a continuous profile.
04
Mitre Cutting
The angle cutter puts the required bevel on each end. Mitred ends let uprights, rails and corner sections seat flush against each other instead of being forced together on site.
05
Precision Drilling
Fixing holes are drilled on the drill-mill centre to fixed positions. Because the hole pattern is machined rather than marked out, frames from different batches still line up with the same fasteners.
06
Finished Part Inspection
Machined aluminium parts are gathered for inspection — length, hole position, mitre angle and edge finish — before anything leaves for coating.
07
Powder Coating
Approved parts go out to our coating partner for powder coating, then return to us for kitting and export packing. Only coated parts that pass re-inspection on return are packed to an order.
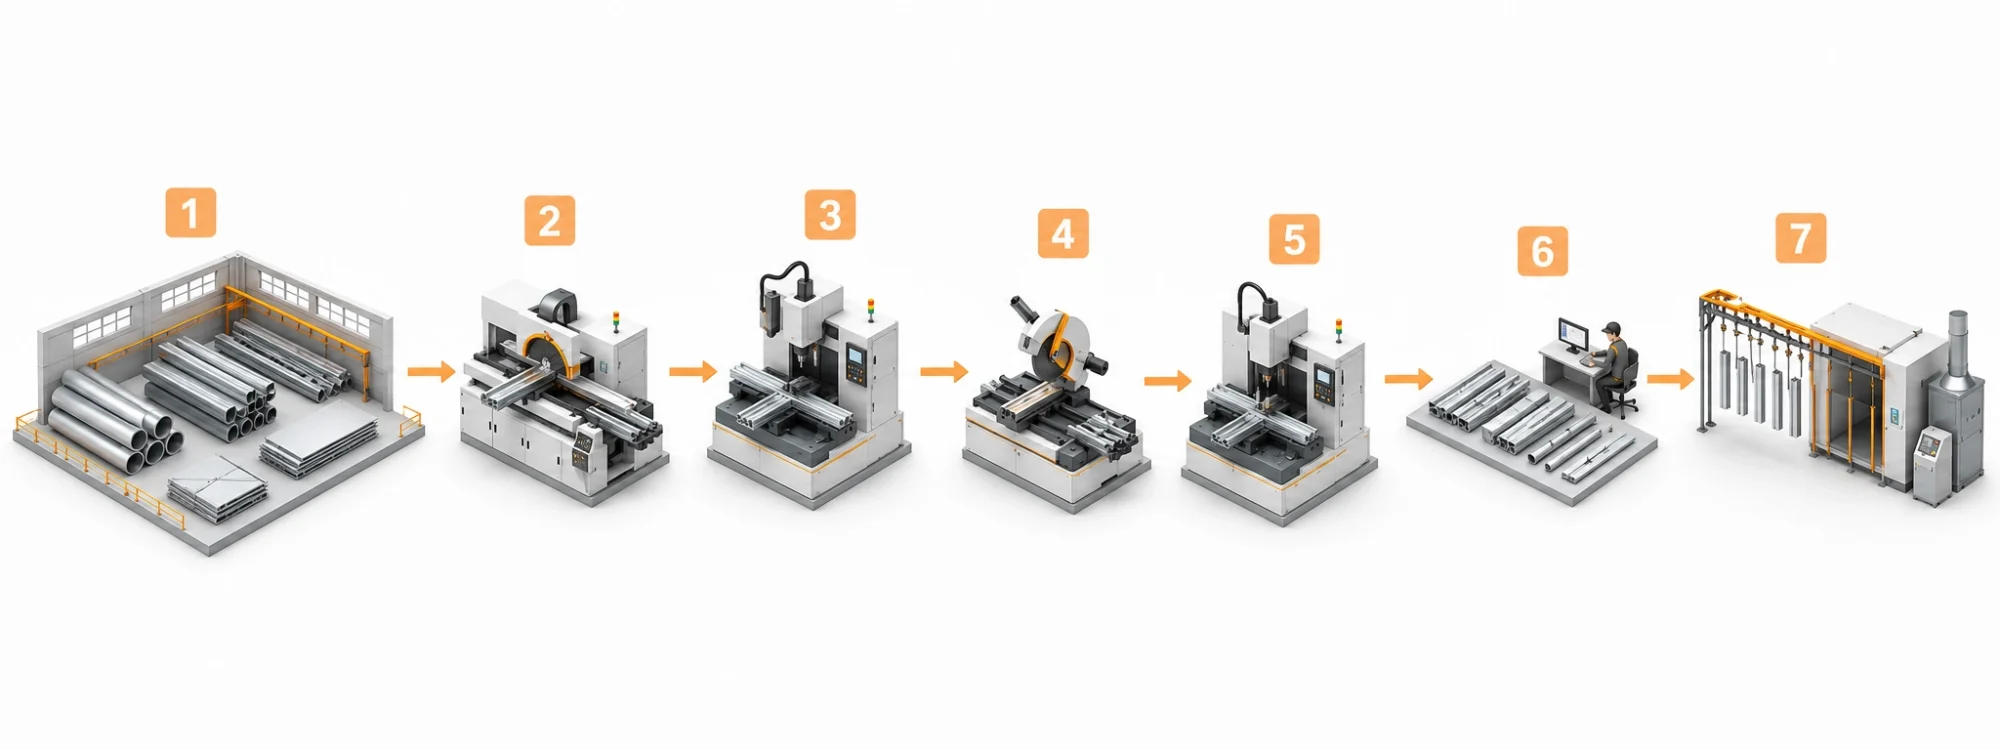
01
Material Intake
Raw material is split into two synchronised streams — sheet to panel forming, tube to cutting — so both run in parallel and converge for assembly.
02
Parallel Routing
Raw material is split into two synchronised streams — sheet to panel forming, tube to cutting — so both run in parallel and converge for assembly.
03
Milling & Deburring
Cut bars go to the drill-mill machine for finish machining, and the saw edge is deburred in the same pass — so nothing sharp or ragged carries through to assembly or to the customer’s hands.Sheet is fed through the roll former to produce corrugated roof and wall panels in a continuous profile.
04
Mitre Cutting
The angle cutter puts the required bevel on each end. Mitred ends let uprights, rails and corner sections seat flush against each other instead of being forced together on site.
05
Precision Drilling
Fixing holes are drilled on the drill-mill centre to fixed positions. Because the hole pattern is machined rather than marked out, frames from different batches still line up with the same fasteners.
06
Finished Part Inspection
Machined aluminium parts are gathered for inspection — length, hole position, mitre angle and edge finish — before anything leaves for coating.
07
Powder Coating
Approved parts go out to our coating partner for powder coating, then return to us for kitting and export packing. Only coated parts that pass re-inspection on return are packed to an order.
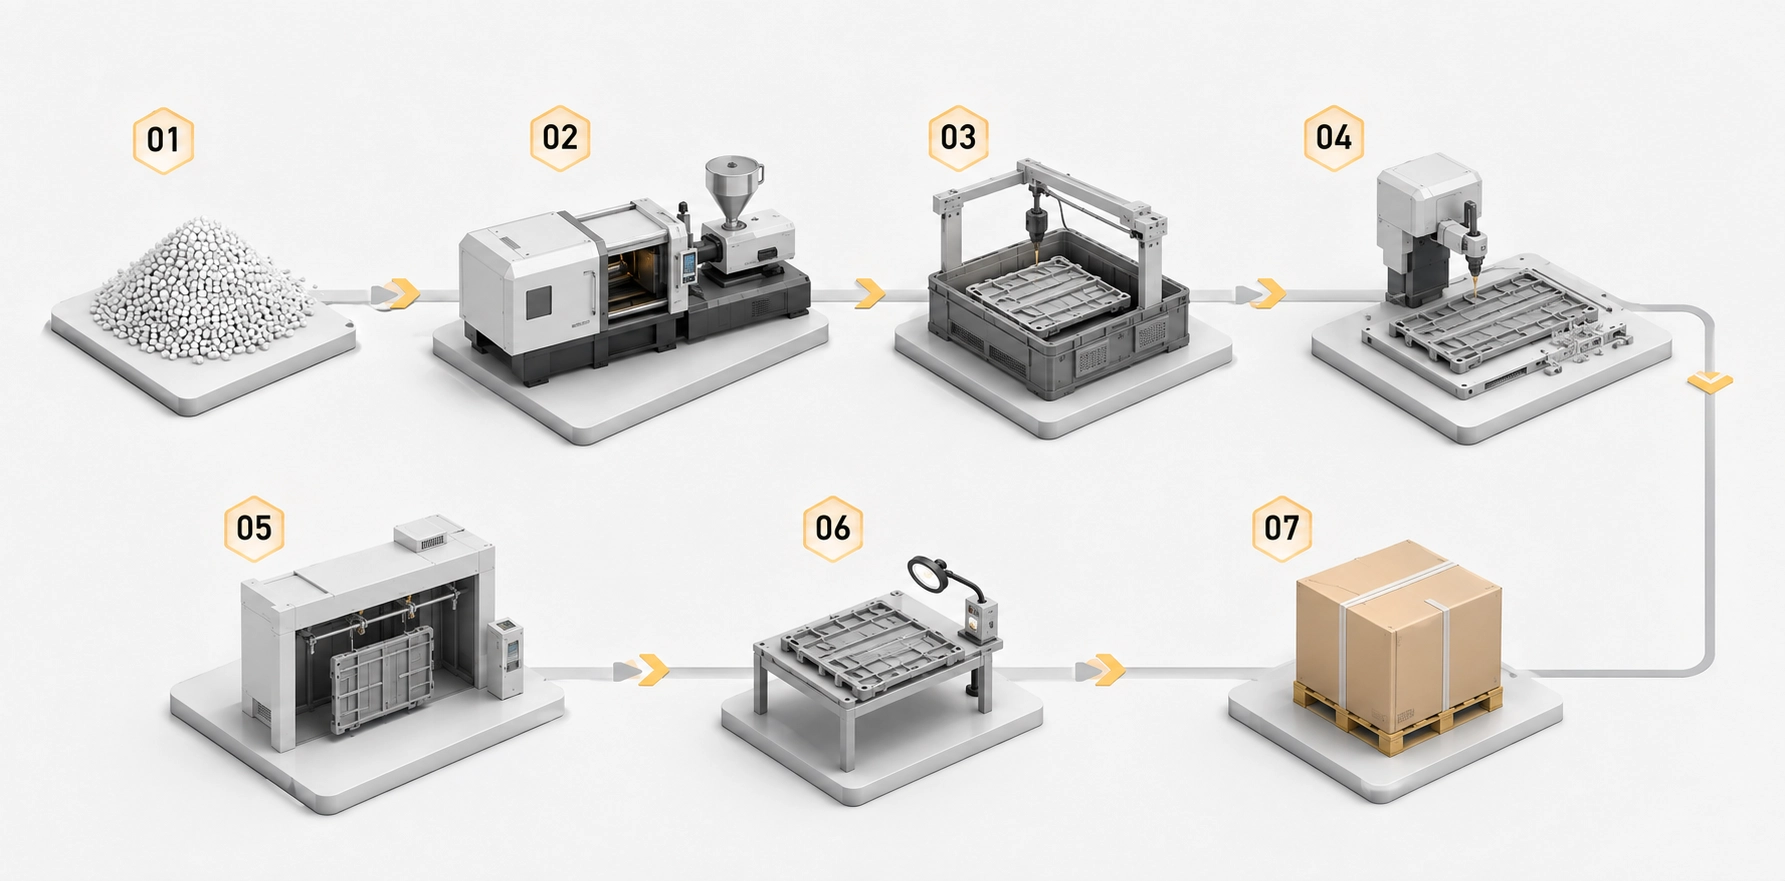
01
Profile Intake
Resin pellets and colour masterbatch are received into the plastics workshop. Material and colour are matched to the order specification before the line is charged.
02
Parallel Routing
Resin pellets and colour masterbatch are received into the plastics workshop. Material and colour are matched to the order specification before the line is charged.
03
Melting & Colour Blending
Pellets are melted at temperature and the masterbatch is blended through the melt, giving colour that runs right through the material rather than sitting on the surface.Sheet is fed through the roll former to produce corrugated roof and wall panels in a continuous profile.
04
Profile Extrusion
The melt is pushed through the extruder die to a fixed panel width and wall section. Changing the die changes the profile, so panel geometry stays repeatable across a production run.
05
Oven Heating & Flattening
Extruded board is passed through the oven and pressed flat while warm, taking out any bow picked up on the way off the line.
06
Double-Head Saw Cutting
Boards are cut to finished length on the double-head saw while still held flat, so both ends come off square and to the same dimension.
07
Surface Brushing
The face is brushed to raise a matt, timber-like texture — the base grain that stops the panel reading as flat plastic.
08
Embossing
Panels pass through the embossing rolls, where the texture tooling is swapped to suit the finish specified for the order. Moulded fittings from the parallel stream rejoin here for consolidated inspection and export packing.Components go to powder coating, then return for kitting and export packing.
What DiBiBi can Physically Make?
Working envelopes for each in-house process. Machine makes and models are withheld under our confidentiality policy and are disclosed during an on-site audit.
| Process | Capability | Working range |
|---|---|---|
| Roll forming | Continuous profile forming | Coil width up to 1,500 mm · thickness 0.3–1.2 mm |
| Stamping / punching | CNC turret punching | Sheet up to 1,500 × 3,000 mm · punching force 30–33 T |
| Bending | CNC press brake | Bending length up to 3,200 mm · tolerance ±0.5 mm |
| Welding | MIG / spot welding | Fixture-controlled assembly |
| Aluminium profile finishing | Cutting, CNC machining, anodizing / powder coating | Profile length up to 6,000 mm |
| Powder coating | Automatic coating line, oven cured | Part size up to 6,000 × 1,500 × 2,000 mm · film thickness 70 ±10 μm |
| PP panel extrusion | Continuous structural panel forming | Panel thickness 16–20 mm |
| PP injection moulding | Structural connectors and reinforced components | Clamping force 300–3,000 T |
Garden Structures
Our Product Lines
We specialize in three core product lines, each engineered to meet the expectations of today’s retail and wholesale buyers.
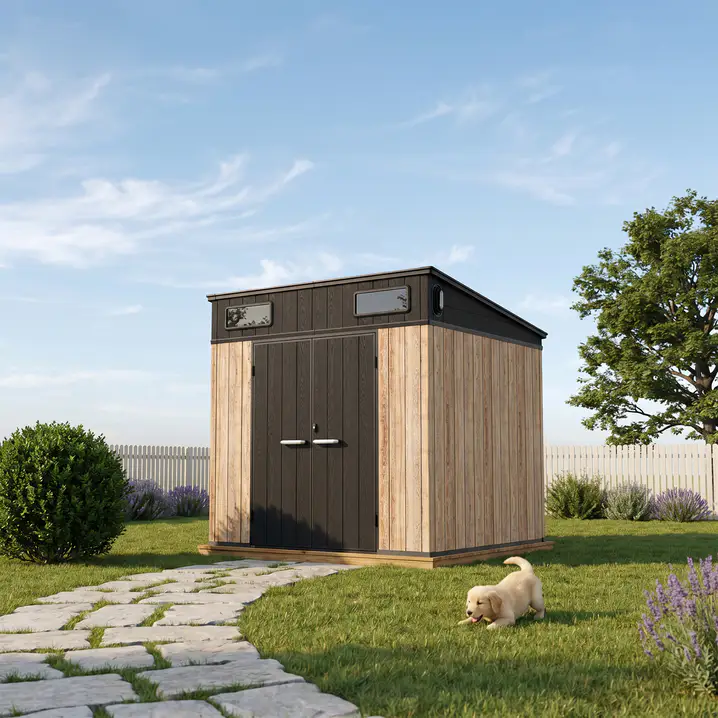
Outdoor Plastic Storage
Available in a full range of sizes, from compact storage to full walk-in structures. Built for durability, easy assembly, and broad SKU coverage.
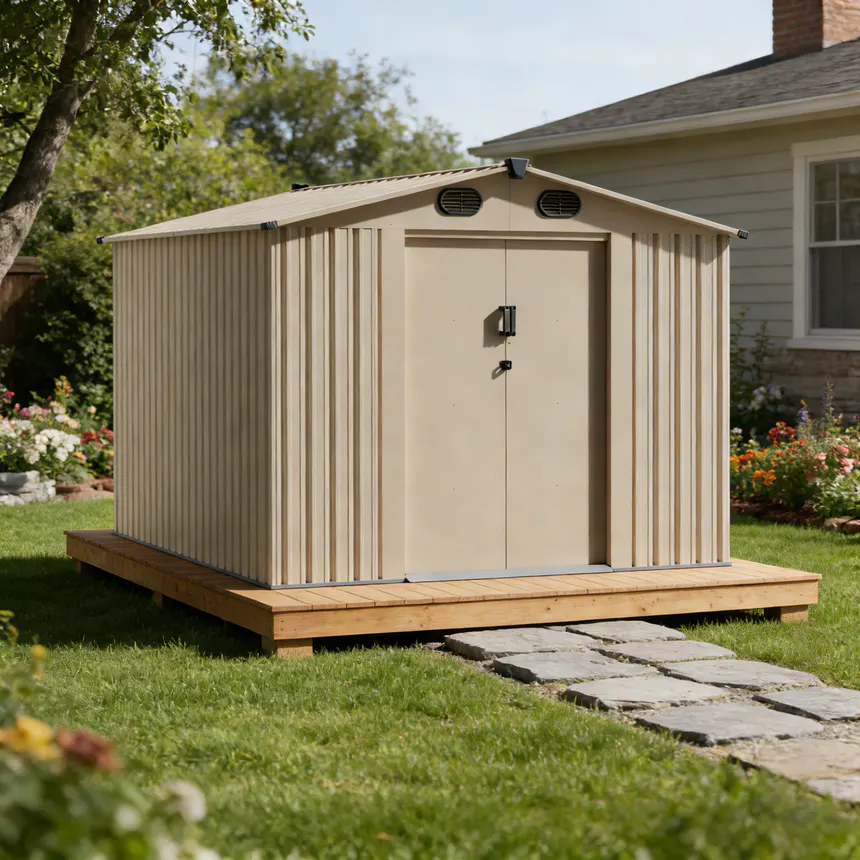
Heavy Duty Metal Storage
Versatile, high-load solutions for garages, commercial spaces, and demanding residential use.
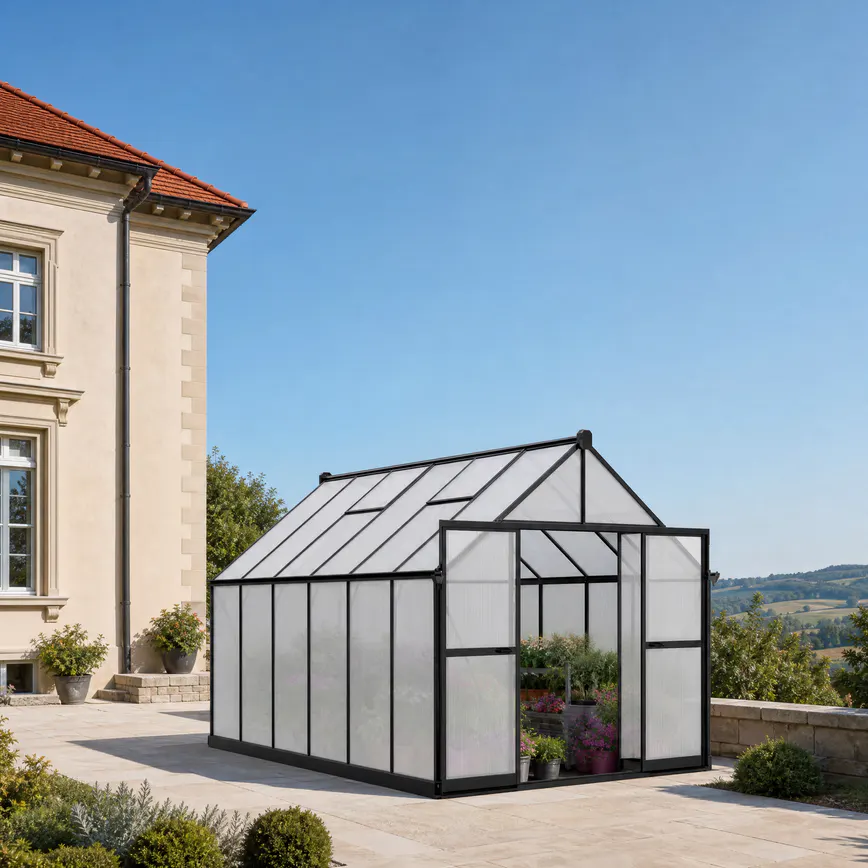
Aluminum Greenhouse
Modern, clean-lined structures that bring design sensibility to the growing garden category. Cold Frame boxes are also available in greenhouse serials.
Inside the operation
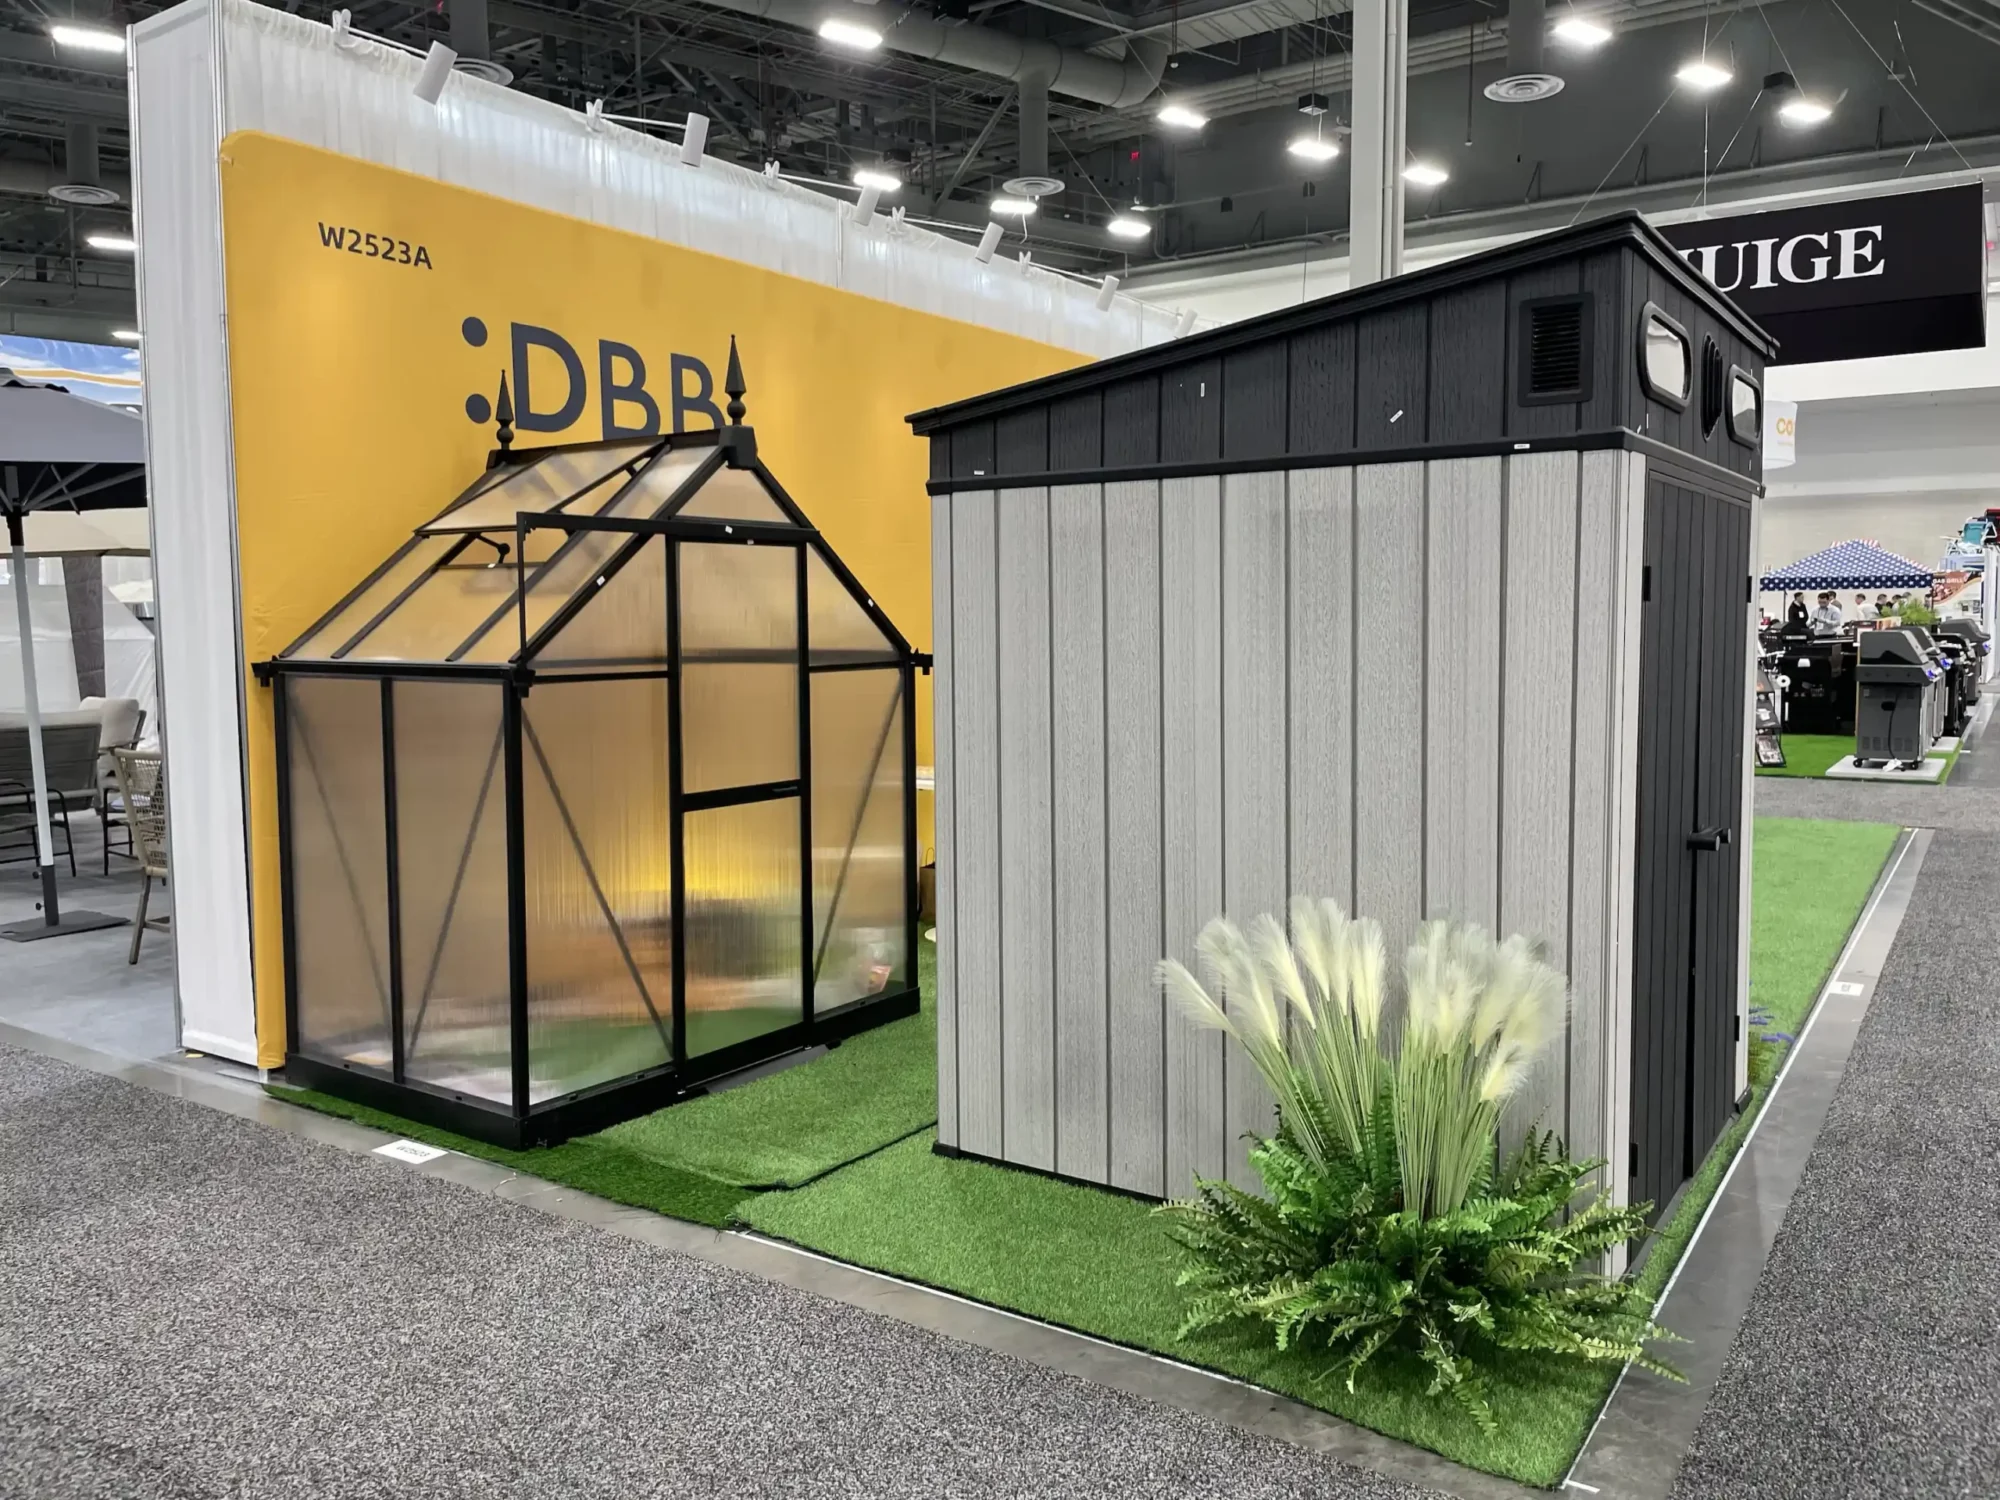
Where DiBiBi Shows Up
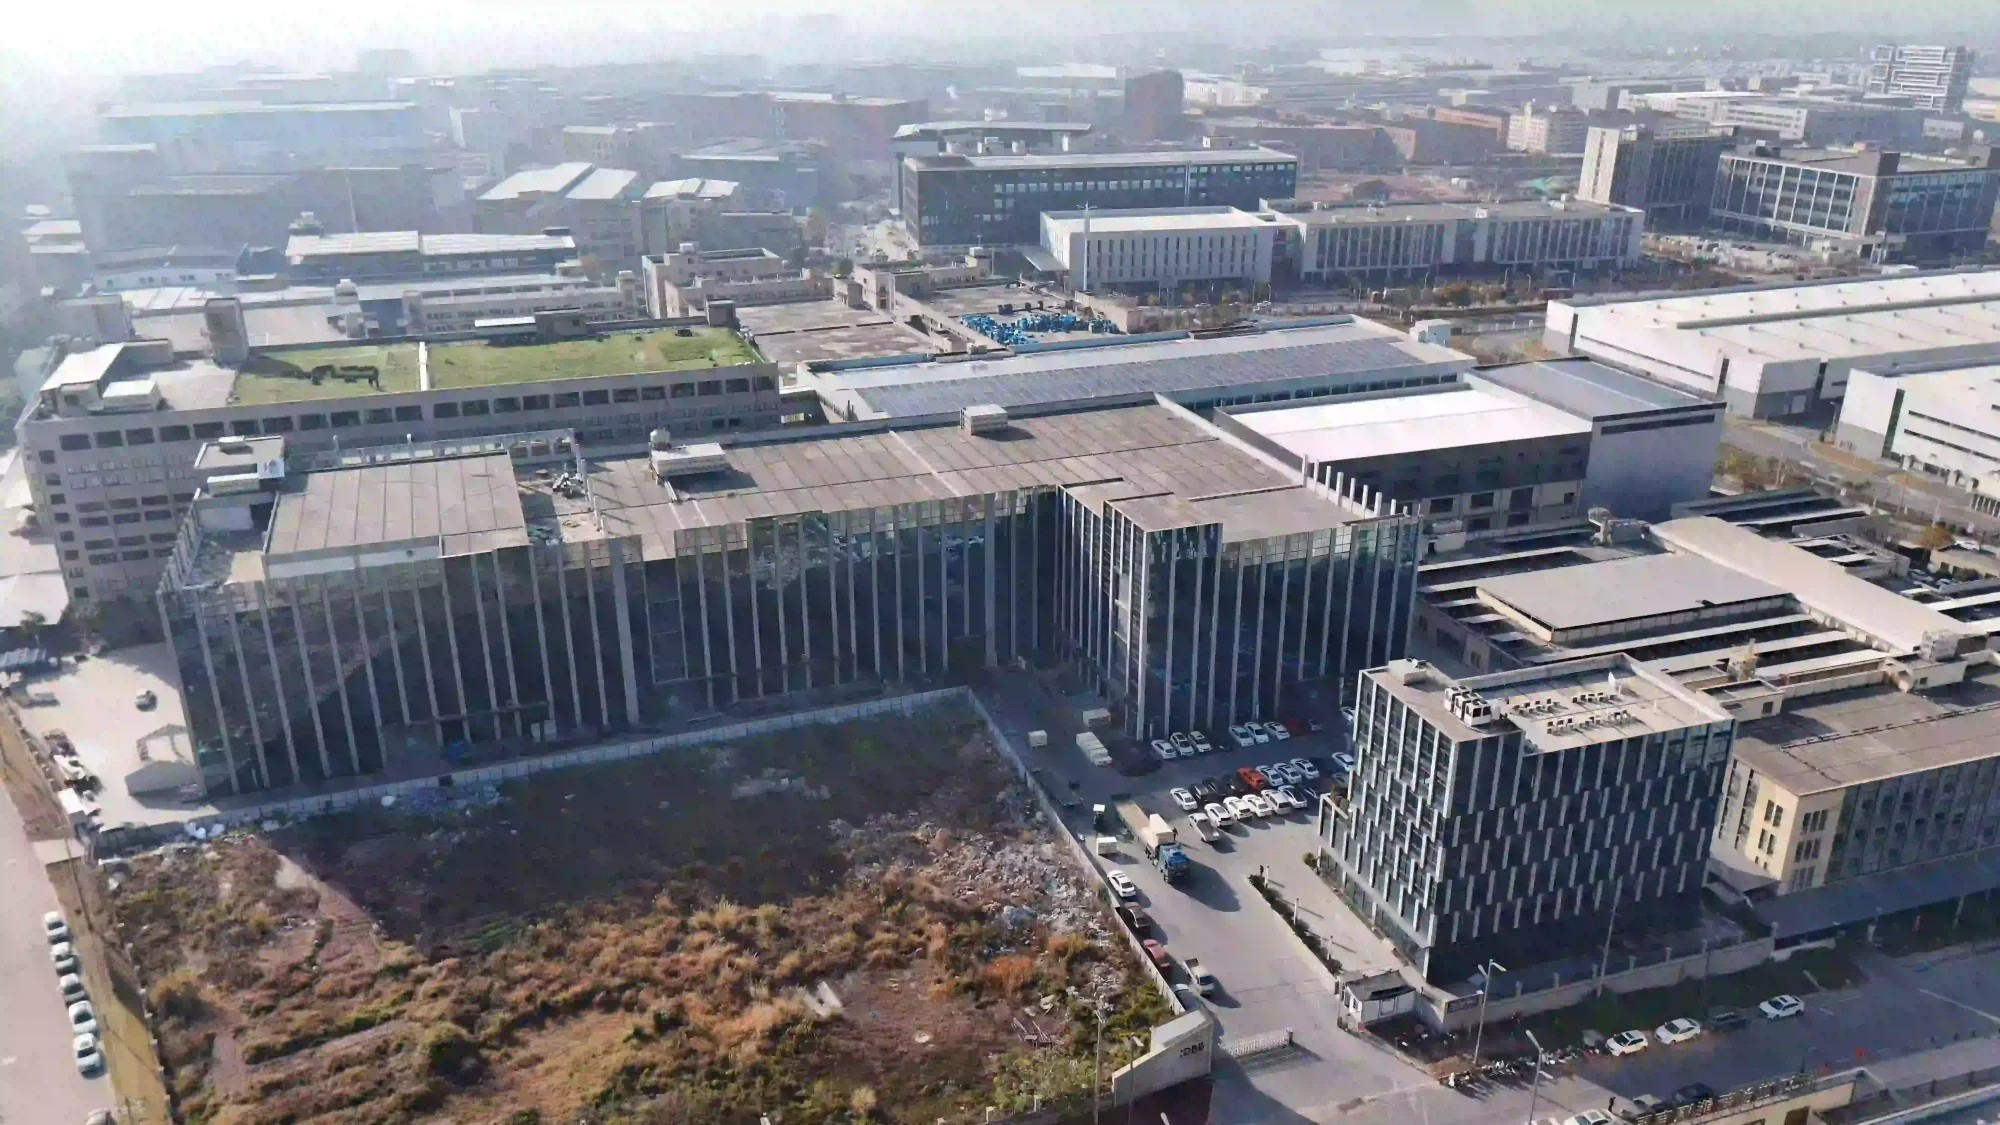
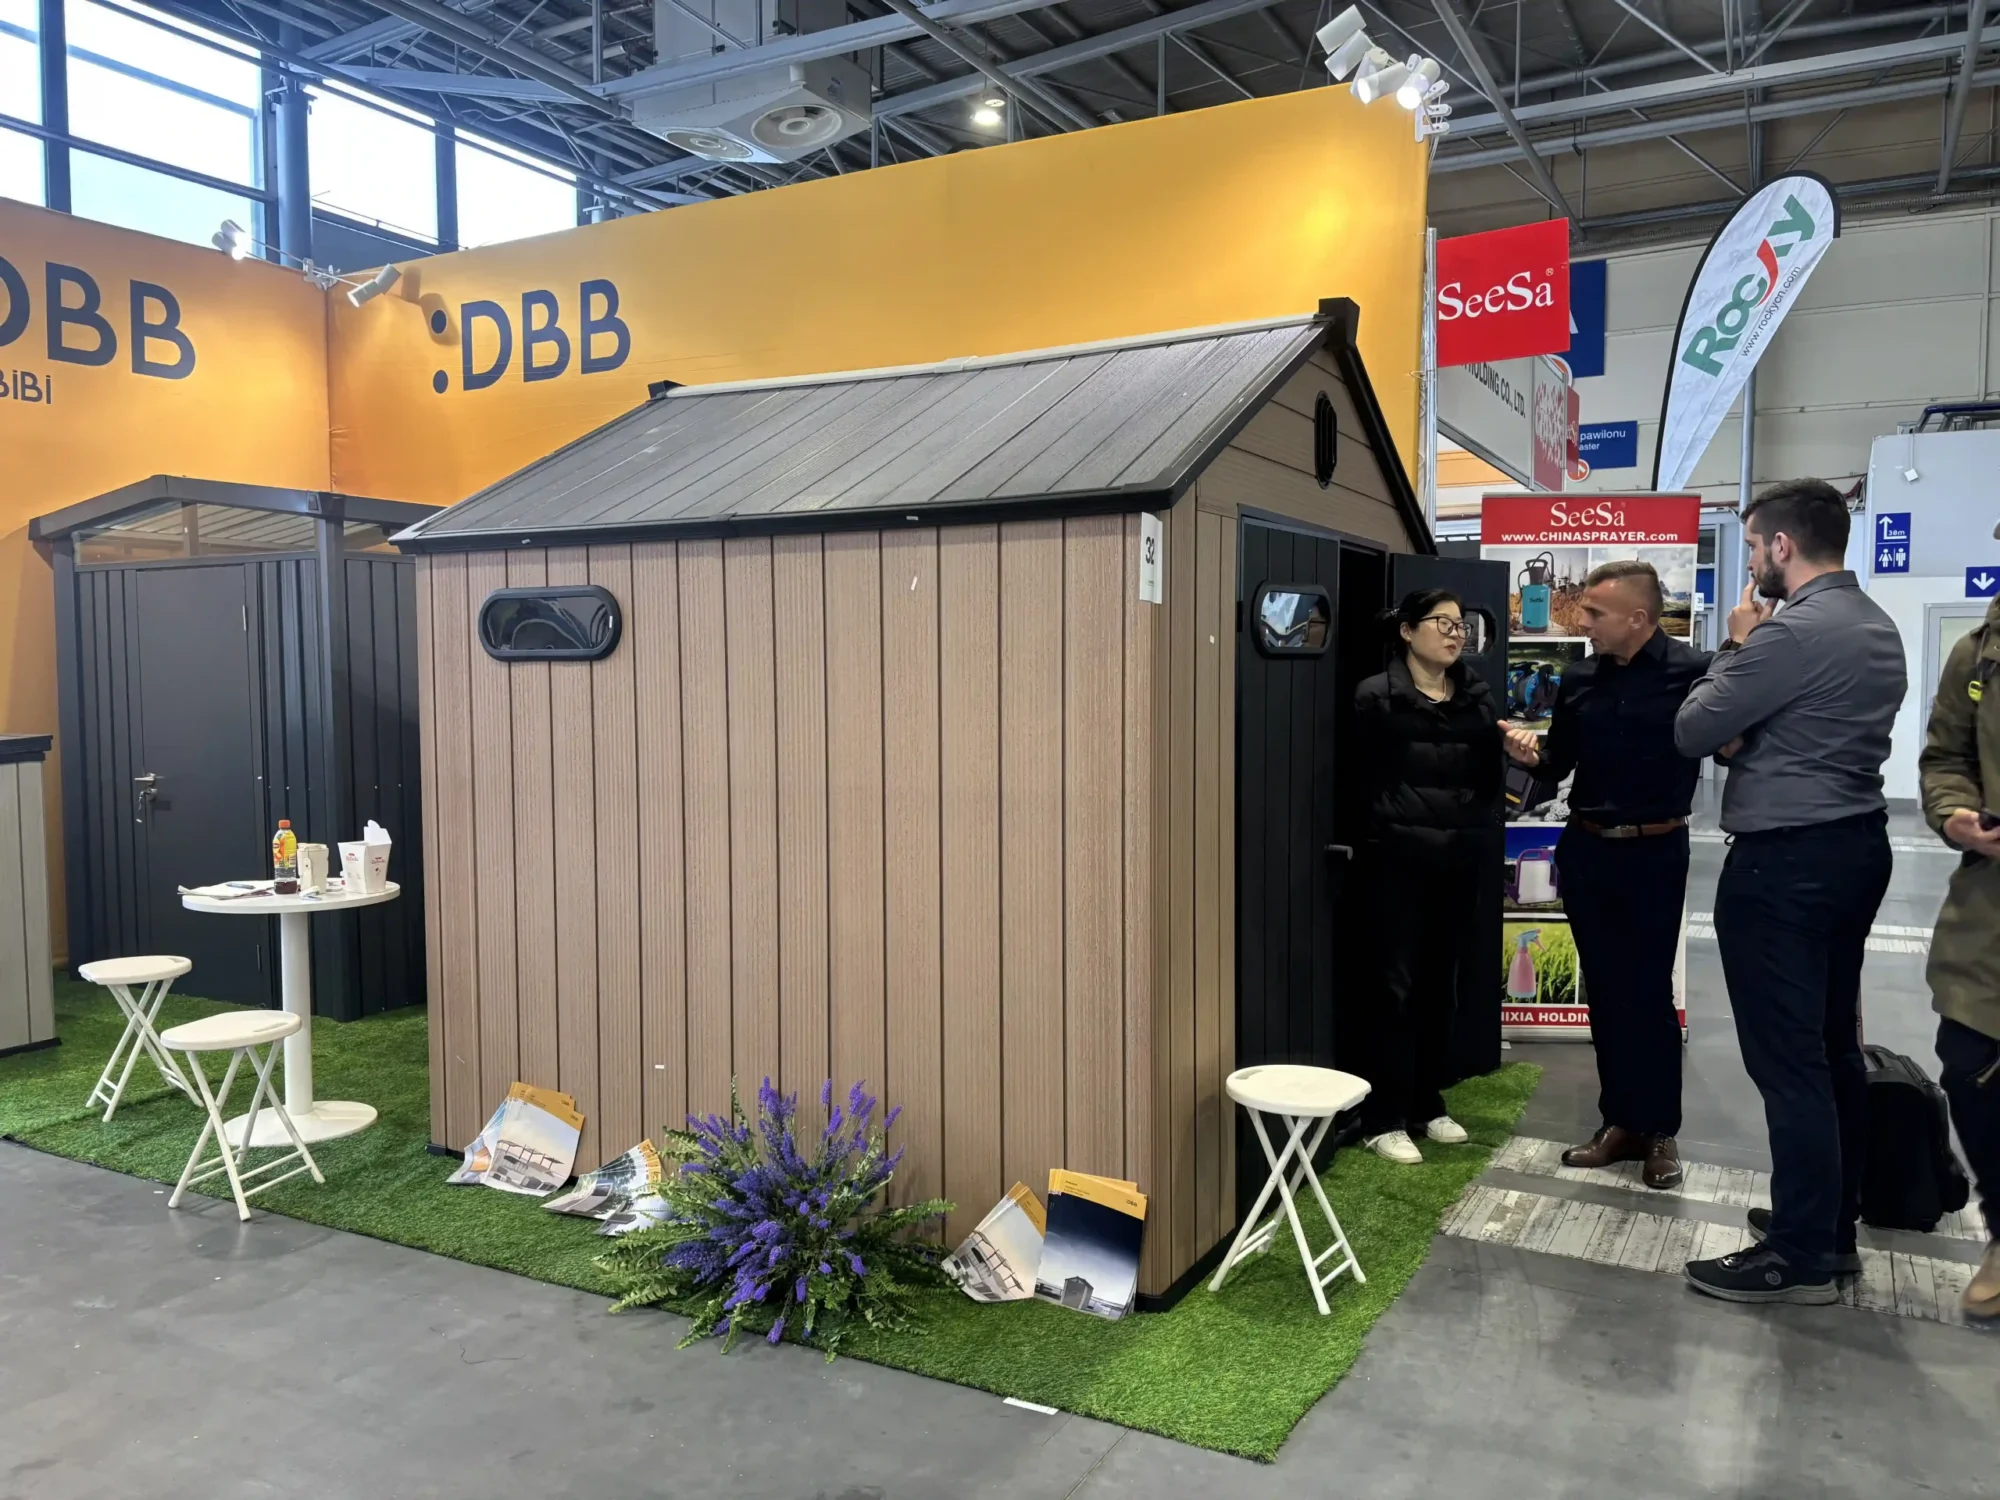
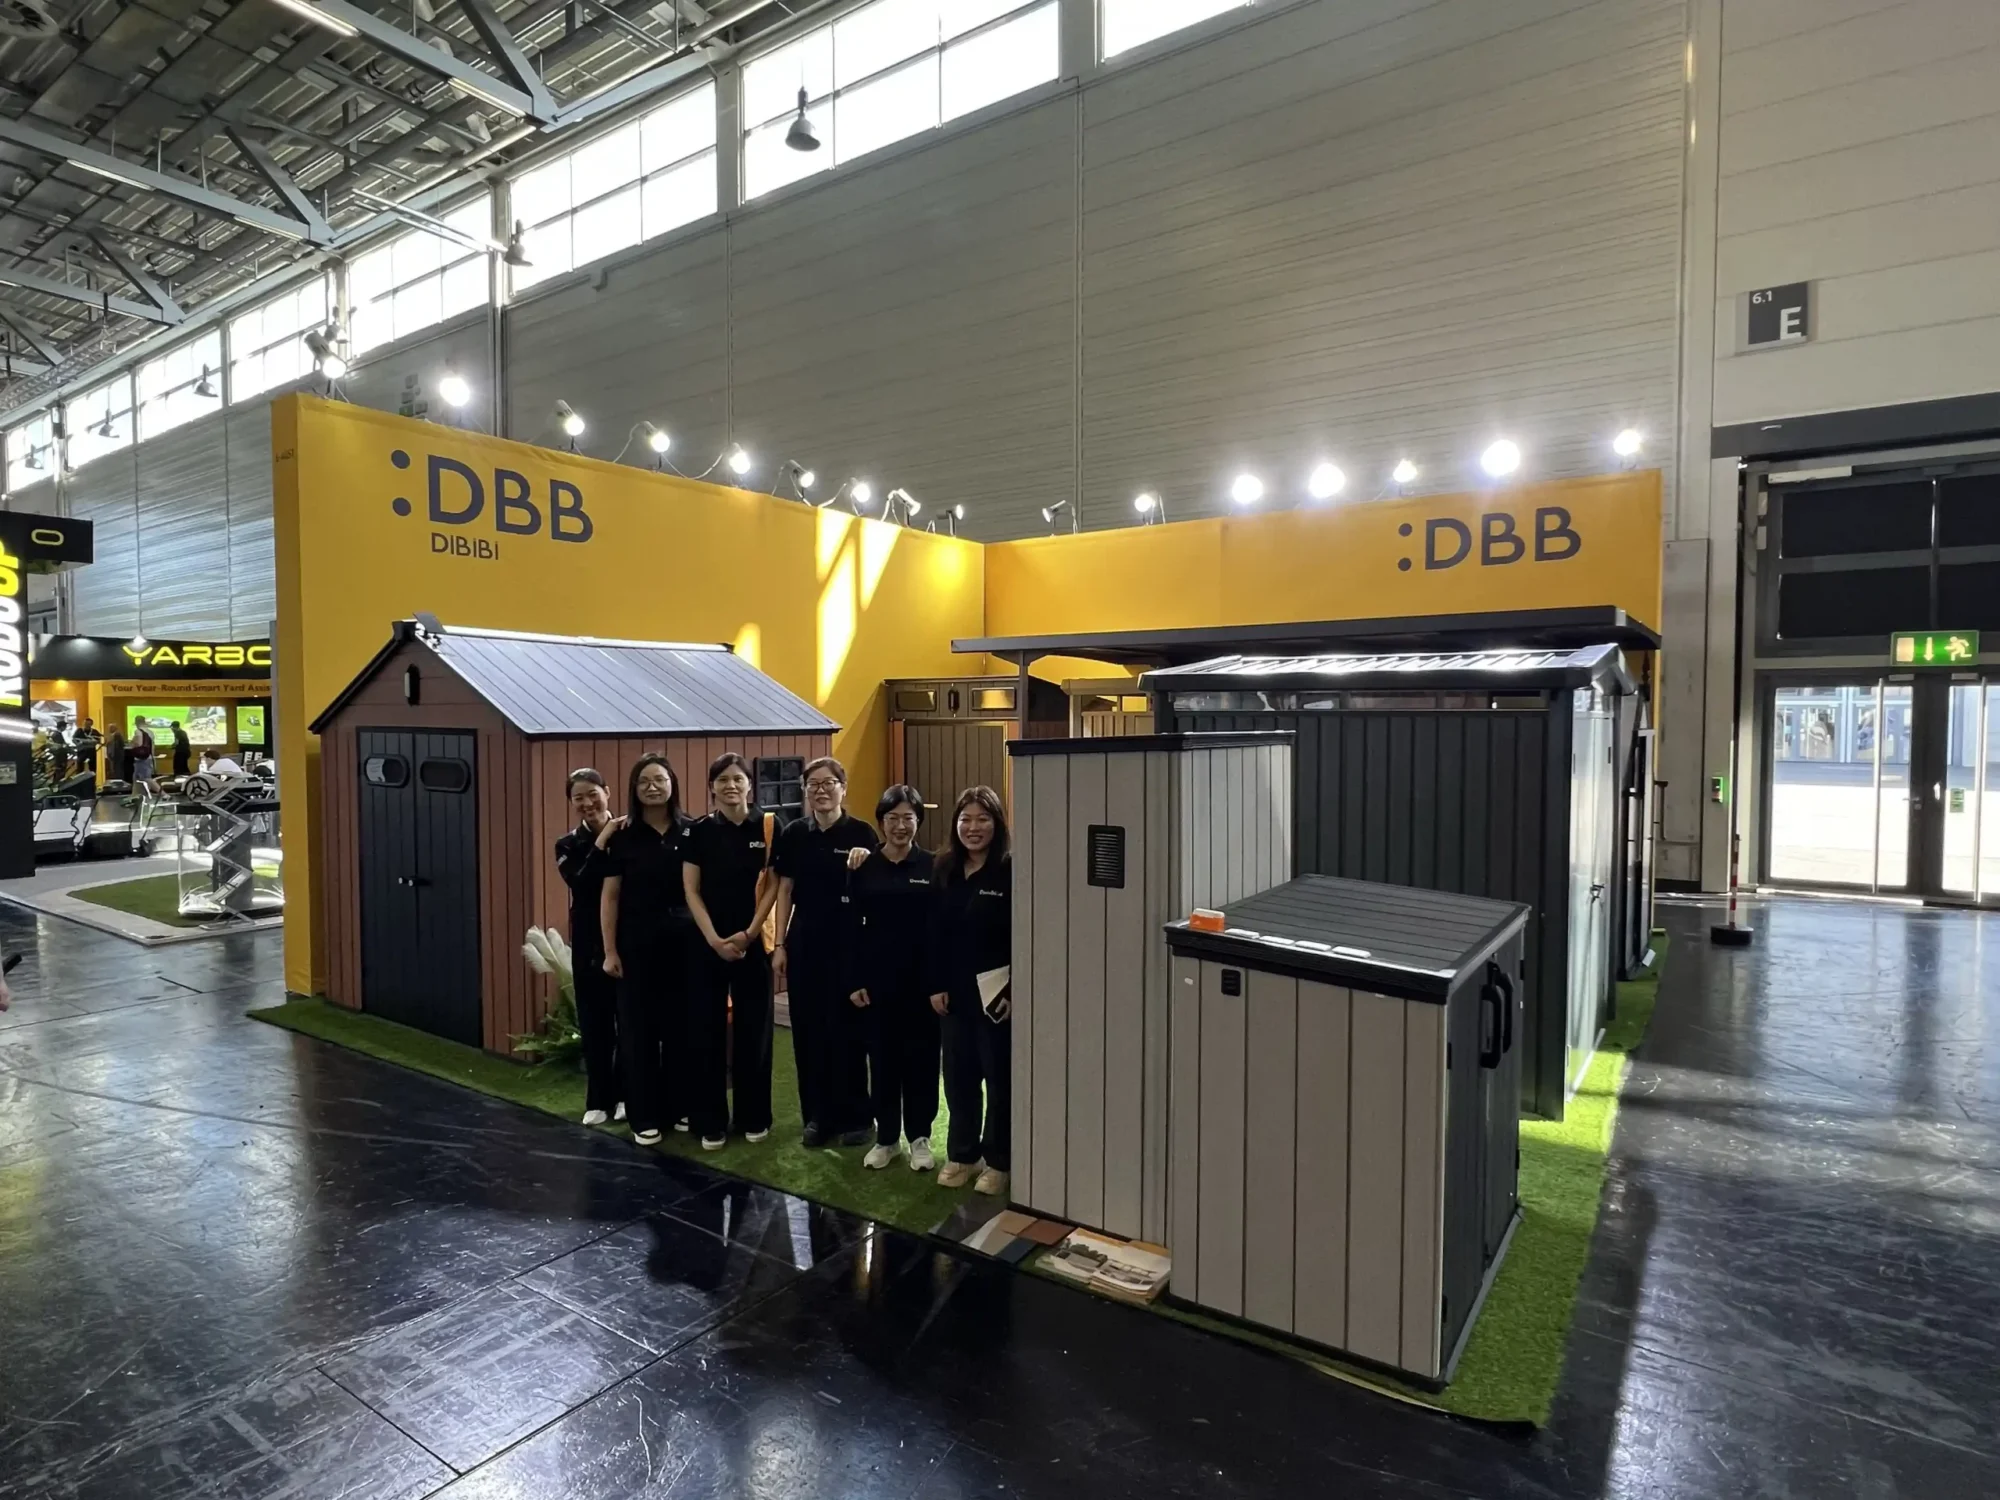
Inside our production floor, innovation labs and trade show booths.
Start your project
Get a quoted BOM in 48 hours.
Send drawings, samples, or just a reference photo. Our engineering team returns tooling cost, unit price at three MOQ tiers, and a lead-time plan — no obligation.
♦ISO 9001 certified
◊ 100,000 m² facility
♦15 yrs experiences
Inquire Now
Please take a moment to fill out the form. we will get back to you ASAP.